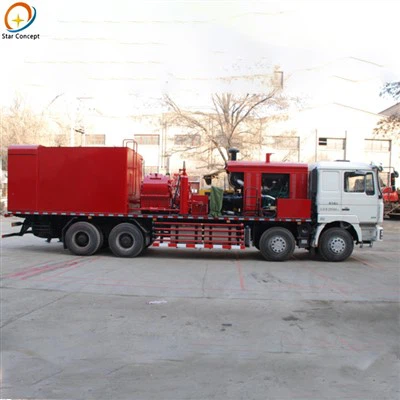
If you’ve ever operated cementing equipment in Denver or worked a job site above 10,000 feet in the Rockies or Andean highlands, you know it’s a whole different game than cementing at sea level. Last month, I spent three weeks troubleshooting cementing operations for a client running surface casing in a remote Wyoming well, and let me tell you—their standard equipment barely made it through the first 48 hours before we had to hit pause to adjust for altitude. As a cementing equipment supplier who’s been doing this for 18 years, I don’t just sell parts and rigs; I’m the guy you call when your cement job starts going sideways because the air’s thin, the pressure’s wonky, and every equation you learned in school seems to break. Today, I want to walk you through exactly how high altitude twists every part of cementing equipment, why our gear is built to fight those twists, and what you need to know to nail a job above 5,000 feet (the point where atmospheric pressure drops enough to matter, by the way). Cementing Equipment
First, let’s get the basics out of the way that no one warns you about: at 1,000 feet above sea level, atmospheric pressure is about 14.7 psi. Jump that to 8,000 feet, and that number plummets to roughly 10.9 psi—almost a 26% drop. For context, that’s the same pressure difference as putting your whole rig on a small hill, not a mountain. Now, cementing isn’t just mixing a bucket of concrete; it’s a precise process where you mix dry cement, water, and additives on-site, pump that slurry down the wellbore, wait for it to set, and make sure it seals the annulus (the gap between the casing and the wellbore wall) to prevent leaks, gas migration, or well blowouts. Every step relies on pressure, density, and chemical reaction rates—all of which go haywire when the air pressure outside your equipment tank is lower.
Let’s start with the core part of any cementing crew: the mixing unit. This is where you dump your cement powder, water, bentonite, accelerators, retarders, and fluid-loss additives, and spin them into a smooth, uniform slurry. At sea level, the mixers work because the suction lines pulling water from the tank generate enough vacuum to draw fluid into the mixing chamber at a steady rate, and the centrifugal force from the spinning impeller keeps the powder from clumping too much. But high altitude kills suction. The lower atmospheric pressure means the differential pressure between the water tank surface and the pump inlet is smaller—so your pump has to work way harder to pull the same volume of water. I’ve seen standard mixers at 9,000 feet take 20 minutes longer to mix a single batch of slurry than they would at sea level, and half the time, you end up with lumpy, aerated slurry. That’s a disaster. Aerated slurry is less dense, which means it can’t exert enough hydrostatic pressure to hold back formation fluids, and it’s way harder to pump down the well.
So, how do we fix that? Our cementing mixing units come with altitude-adjusted water pumps and modified suction lines. We install priming assist pumps that create a small, controlled vacuum at the pump inlet, boosting that differential pressure even at 10,000 feet, so the water flows consistently. We also add adjustable impeller speeds—at lower altitudes, you run the impeller at full tilt to avoid air entrainment, but at high altitude, you drop the speed by 10-15% to keep from whipping air into the slurry, while still spinning fast enough to break down clumps. Last year, a client in Peru’s Andes at 11,500 feet used our modified mixing unit and cut their mix time by 40%, and their slurry density stayed within 0.2 ppg of their target the whole job—something their old off-the-shelf mixer never pulled off.
Next up: the cement pumps. These are the workhorses of the operation, pumping the mixed slurry at high pressure down the casing. At sea level, pump performance is rated for a certain flow rate and pressure, but high altitude doesn’t care about those factory specs. Wait—no, actually, it does care, but only if you don’t adjust. The key here is that pump discharge pressure has to work against two things: the hydrostatic pressure of the slurry itself and the backpressure from the wellbore and formation. But at high altitude, the lower atmospheric pressure means the total pressure you need to push the slurry is different than at sea level. Wait, let’s get technical for a second: the hydrostatic pressure of a slurry is calculated by its density multiplied by gravity multiplied by depth (P = ρgh). Gravity is constant, so why does altitude matter? Because the pump’s intake side is open to the atmosphere, so the absolute pressure at the pump inlet is lower. If the pump is positive displacement (which most cement pumps are), its output is a function of displacement per stroke, inlet pressure, and outlet pressure. Lower inlet pressure means you get less flow per stroke unless you adjust the pump’s stroke rate or pressure settings.
Standard cement pumps are calibrated for sea level, so at 8,000 feet, you might notice the pump is hitting its pressure limit 500 psi earlier than expected, even when the slurry is the same density. That’s not the pump failing—it’s just not accounting for the lower atmospheric pressure robbing the inlet side. Our pumps come with built-in altitude compensation modules that adjust the stroke rate and pressure setpoint automatically when you input the job site elevation. No more manually tweaking pressure gauges with a calculator that’s probably wrong because you forgot to account for temperature (another big factor in high altitudes—daily temperature swings of 30 degrees or more change slurry viscosity, which changes pump backpressure). I had a client in Montana last winter who was running a job at 7,500 feet; his old pump would stall every time he pushed past 10 barrels per minute, but with our altitude module, he pumped 18 barrels per minute without a hiccup, finishing the job two days ahead of schedule.
Now, let’s talk about one of the trickiest parts: slurry testing and additives. Even if your equipment works, if your slurry isn’t formulated for high altitude, you’re sunk. Here’s why: the rate of cement hydration (the chemical reaction that makes cement harden) changes with pressure and temperature, but high altitude messes with that too? Wait, no—actually, it’s more about the surface conditions. At lower atmospheric pressure, the water in the slurry can evaporate faster if it’s left sitting, which changes the slurry density. Also, the time it takes for the cement to start setting (the thickening time) is different. At sea level, if you add a retarder, you get 2 hours of thickening time, but at 10,000 feet, that same retarder might only give you 45 minutes—because the lower pressure speeds up the reaction? Wait, no, actually, it’s a mix of pressure and temperature, but our equipment suppliers work closely with cement chemists to adjust our equipment’s on-site testing tools. We add portable densiometers that are calibrated for altitude, because a standard densiometer assumes a reference atmospheric pressure of 14.7 psi—at 10,000 feet, that calibration is off, so you’ll measure a slurry as less dense than it actually is. That leads to under-pressuring the well, which can cause gas migration into the cement before it sets.
I can tell you a story about a client in Colorado a few years back who skipped using our calibrated densiometer. They used their old one from a Texas job, and measured slurry density as 15.8 ppg, but it was actually 16.2 ppg—they just needed to adjust for the 5,280-foot elevation. They pumped the slurry down, and because the actual density was higher, the hydrostatic pressure was too high, which cracked the casing. That cost them $200k in repairs and a week of downtime. Since then, every high-altitude client I work with gets a free set of altitude-calibrated testing tools, and I walk their crew through how to use them on-site.
Another big one: air entrainment and pressure control on the return side. When you pump the cement slurry down the casing, the displaced fluid (usually drilling mud) comes back up the annulus, and you have to control the return pressure to make sure you don’t have backpressure that’s too high or too low. At high altitude, the return lines are open to the atmosphere, so the pressure at the annulus surface is lower, which can cause the drilling mud returning to aerate as it flows through the surface lines. Aerated return fluid makes it hard to measure the flow rate, and it can also lead to sudden pressure spikes that blow out pressure relief valves. Our cementing equipment includes return line scrubbers that remove entrained air from the returning fluid before it hits the flow meters, so you get accurate flow data, and pressure relief valves that are calibrated for altitude—they open at a lower pressure setpoint at high elevation, because the atmospheric pressure is lower, so you don’t get unintended pressure releases.
Wait, let’s also talk about something most people don’t consider: cold high-altitude temperatures. A lot of high-altitude job sites are also cold, even in the summer. Slurry viscosity goes up when it’s cold, which means your pumps have to work harder, and mixing takes longer. Our equipment has heated water lines for the mixing unit, so you can adjust the water temperature on-site to keep the slurry viscosity consistent, regardless of how cold it is outside. In the Rockies, I’ve seen temperatures drop to 20 degrees Fahrenheit at 8,000 feet during a night shift, and with our heated lines, the crew never had to pause mixing because the water was too cold.
Now, I know what a lot of crew chiefs are thinking: “This sounds like a lot of extra stuff, and I don’t want to pay for specialized equipment.” Let me be clear: cutting corners on high-altitude cementing equipment isn’t cheap. The job I mentioned earlier in Wyoming where the client almost had a blowout? They tried renting standard equipment from a big-box rental company, and when they called me, they were already two days behind schedule, had to pay for emergency additive shipments, and still ended up needing our modified equipment to finish. Total cost for their delays? Over $500k. The cost of investing in altitude-adjusted cementing equipment? A fraction of that.
What’s the takeaway here? Cementing isn’t one-size-fits-all. The physics of pressure, density, and reaction rates change when you’re above 5,000 feet, and every part of your equipment has to adapt. Standard mixers, uncalibrated pumps, and generic testing tools just don’t work. As a cementing equipment supplier who’s specialized in high-altitude operations for almost two decades, I don’t sell gear that’s designed for sea level and then tweaked with a sticker. We build the altitude adjustment right into every component—from the suction pumps to the pressure modules to the testing tools—so your crew can show up to a remote mountain well, set up in a few hours, and get on with the job without pausing every 30 minutes to adjust settings or troubleshoot.
If you’re gearing up for a high-altitude cement job, or you’ve had a bad experience with equipment that couldn’t handle thin air, I can help. We work with small independent operators and big oil companies alike, and we can either retrofit your existing equipment for altitude or supply you with a full unit that’s tested and calibrated for any elevation up to 15,000 feet. I don’t do pressure washing demos or fancy sales pitches—just honest advice from someone who’s spent more nights on remote job sites than in an office, and knows exactly what goes wrong when altitude messes with your cement job.

So, if you’re ready to stop fighting thin air and start nailing your next high-altitude cement job, reach out to connect for a procurement discussion. We can chat through your site elevation, job size, and challenges, and put together a plan that works for you.
High Pressure Fluid Control Parts References
Bradley, H. B. (1992). Well Control Operations. PennWell Books.
Ewy, R. T. (2003). Cement Slurry Density and Pressure Calculations in High-Altitude Wellbores. SPE Drilling & Completion, 18(4), 264-271.
Mays, L. W. (1999). Hydraulics and Hydraulic Systems. McGraw-Hill.
Nenniger, J. P., & Piro, P. (2018). Cementing in High-Altitude Environments: Key Pressure and Hydration Adjustments. Journal of Petroleum Technology, 70(6), 52-57.
Dongying Star Concept Petroleum Equipment Co., Ltd.
We are one of the most professional cementing equipment manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy durable cementing equipment made in China here from our factory. Good service and quality products are available.
Address: No. 9 Xisi Road, Dongying City, Shandong Province, China
E-mail: ellen@starconcept.cn
WebSite: https://www.star-cementing.com/
